Rated capacity isn’t effective capacity
Rated capacity is what a machine can do while it’s running, fed and unblocked. Effective capacity is what the line ships over a week, a season or a year. Between the two sit losses that a capacity spreadsheet usually folds into one planning factor.
- Interrupts. A hundred one-minute stops and one hundred-minute stop cost the same minutes, but very different throughput once there’s storage between machines.
- Blocking and starving. A stopped machine idles its neighbors, and how far the stop travels depends on the buffers between them. See starved vs blocked.
- Changeovers and mix. Size, flavor, label and allergen changes are part of the schedule. A schedule that’s efficient for one product mix can be badly wrong for another.
- Rate against reliability. Running faster makes more product until failures that rise with rate eat the gain, so output has an optimum speed.
- Seasonality. A plant sized for average demand is idle part of the year and constrained the rest. The useful question is capacity during the peak, given how the line actually behaves.
Those losses don’t add up neatly. Five 85% machines in series can make a 44% line (is 85% OEE achievable?), and arithmetic on averages makes spreadsheet capacity plans come out predictably high. Throughput vs capacity works through the distinction.
The constraint is rarely where the plan puts it
A capacity plan usually names a bottleneck and sizes everything around it. The project record on this site keeps showing that the named bottleneck isn’t the one deciding throughput.
- At a specialty olive packer, a full-plant model confirms the pitting bottleneck and finds other choke points downstream in packaging. Scheduling rules tested in the model raise throughput 15% with no new equipment, and the team tests proposed capital against it before committing it.
- A craft brewery planning to add kegging and bottling finds that neither new line is the limit. Either would over-run the fermenting and serving tanks unless capacity is added there first.
- In a coffee Make-Store-Pack operation, changing packaging size moved the bottleneck, which defeats any plan built around a fixed constraint.
The real constraint was already installed and already looked adequate for the mix the plant ran before. Finding it means running the whole line with the change in place. Finding the hidden bottleneck covers the mechanics.
Capex, overtime or reliability: three ways to buy capacity
When a line falls short of the volume, there are three broad ways to close the gap, usually argued in different meetings with different numbers.
Buy equipment
A second machine, another line, or more storage. It’s durable and expensive, and only worth it if it relieves the stage that’s actually binding.
Buy hours
Overtime, an added shift, or weekend runs. They’re quick to start and easy to reverse, but every added hour runs at the line’s current efficiency, losses included. Asset efficiency vs OEE
Recover capacity
Fix the failure mode that costs the most output, resize a buffer, decouple two stages, change the scheduling rule. This is often the cheapest option, and the hardest to size without a model.
A simulation puts all three on the same footing. A specialty chemicals plant asks how many new bag lines to buy against how much overtime to accept. The model answers over a ten-year horizon, splitting each bag line’s weekly hours into production, repair, changeover, idle and overtime. It also shows that short-term storage between bulk production and packaging would decouple two operations the layout ties together, which surfaces low-capital growth options nobody had costed.
Decoupling is the lever most often missed. A cereal plant stabilizes partially cooked grit so it can be stored and later reconstituted, instead of throttling its cookers to what the toasting ovens can take. The model sizes that at 19.8% more effective production in key demand periods, with no new cooking or oven capacity. It’s a peak-period figure, since in a slack period there’s nothing to recover.
The same comparison works at machine level, weighing a second machine against a reliability improvement on the first. It’s one of the five decisions every production system faces.
New plants and consolidations
Capacity mistakes are most expensive before anything is built. A soap manufacturer consolidating several plants and more than 300 products into one facility uses a model to predict the buffer size between processing and packaging. The model also finds that one planned set of machine assignments leaves material in the system too long, a quality problem that would need a $4 million retrofit. Alternative routings are tested in the model instead, and the company now requires a simulation study before any major capital expenditure.
Spreadsheet capacity model or line simulation?
| Question | Rough-cut spreadsheet | Line simulation |
|---|---|---|
| What it uses | Average rates, availability and a planning factor | Per-failure-mode distributions, buffers, conversions and sequence |
| How losses combine | Added or multiplied as if independent | Emerge from the line running through time |
| Where the constraint is | An input assumption | An output, which can move with the mix |
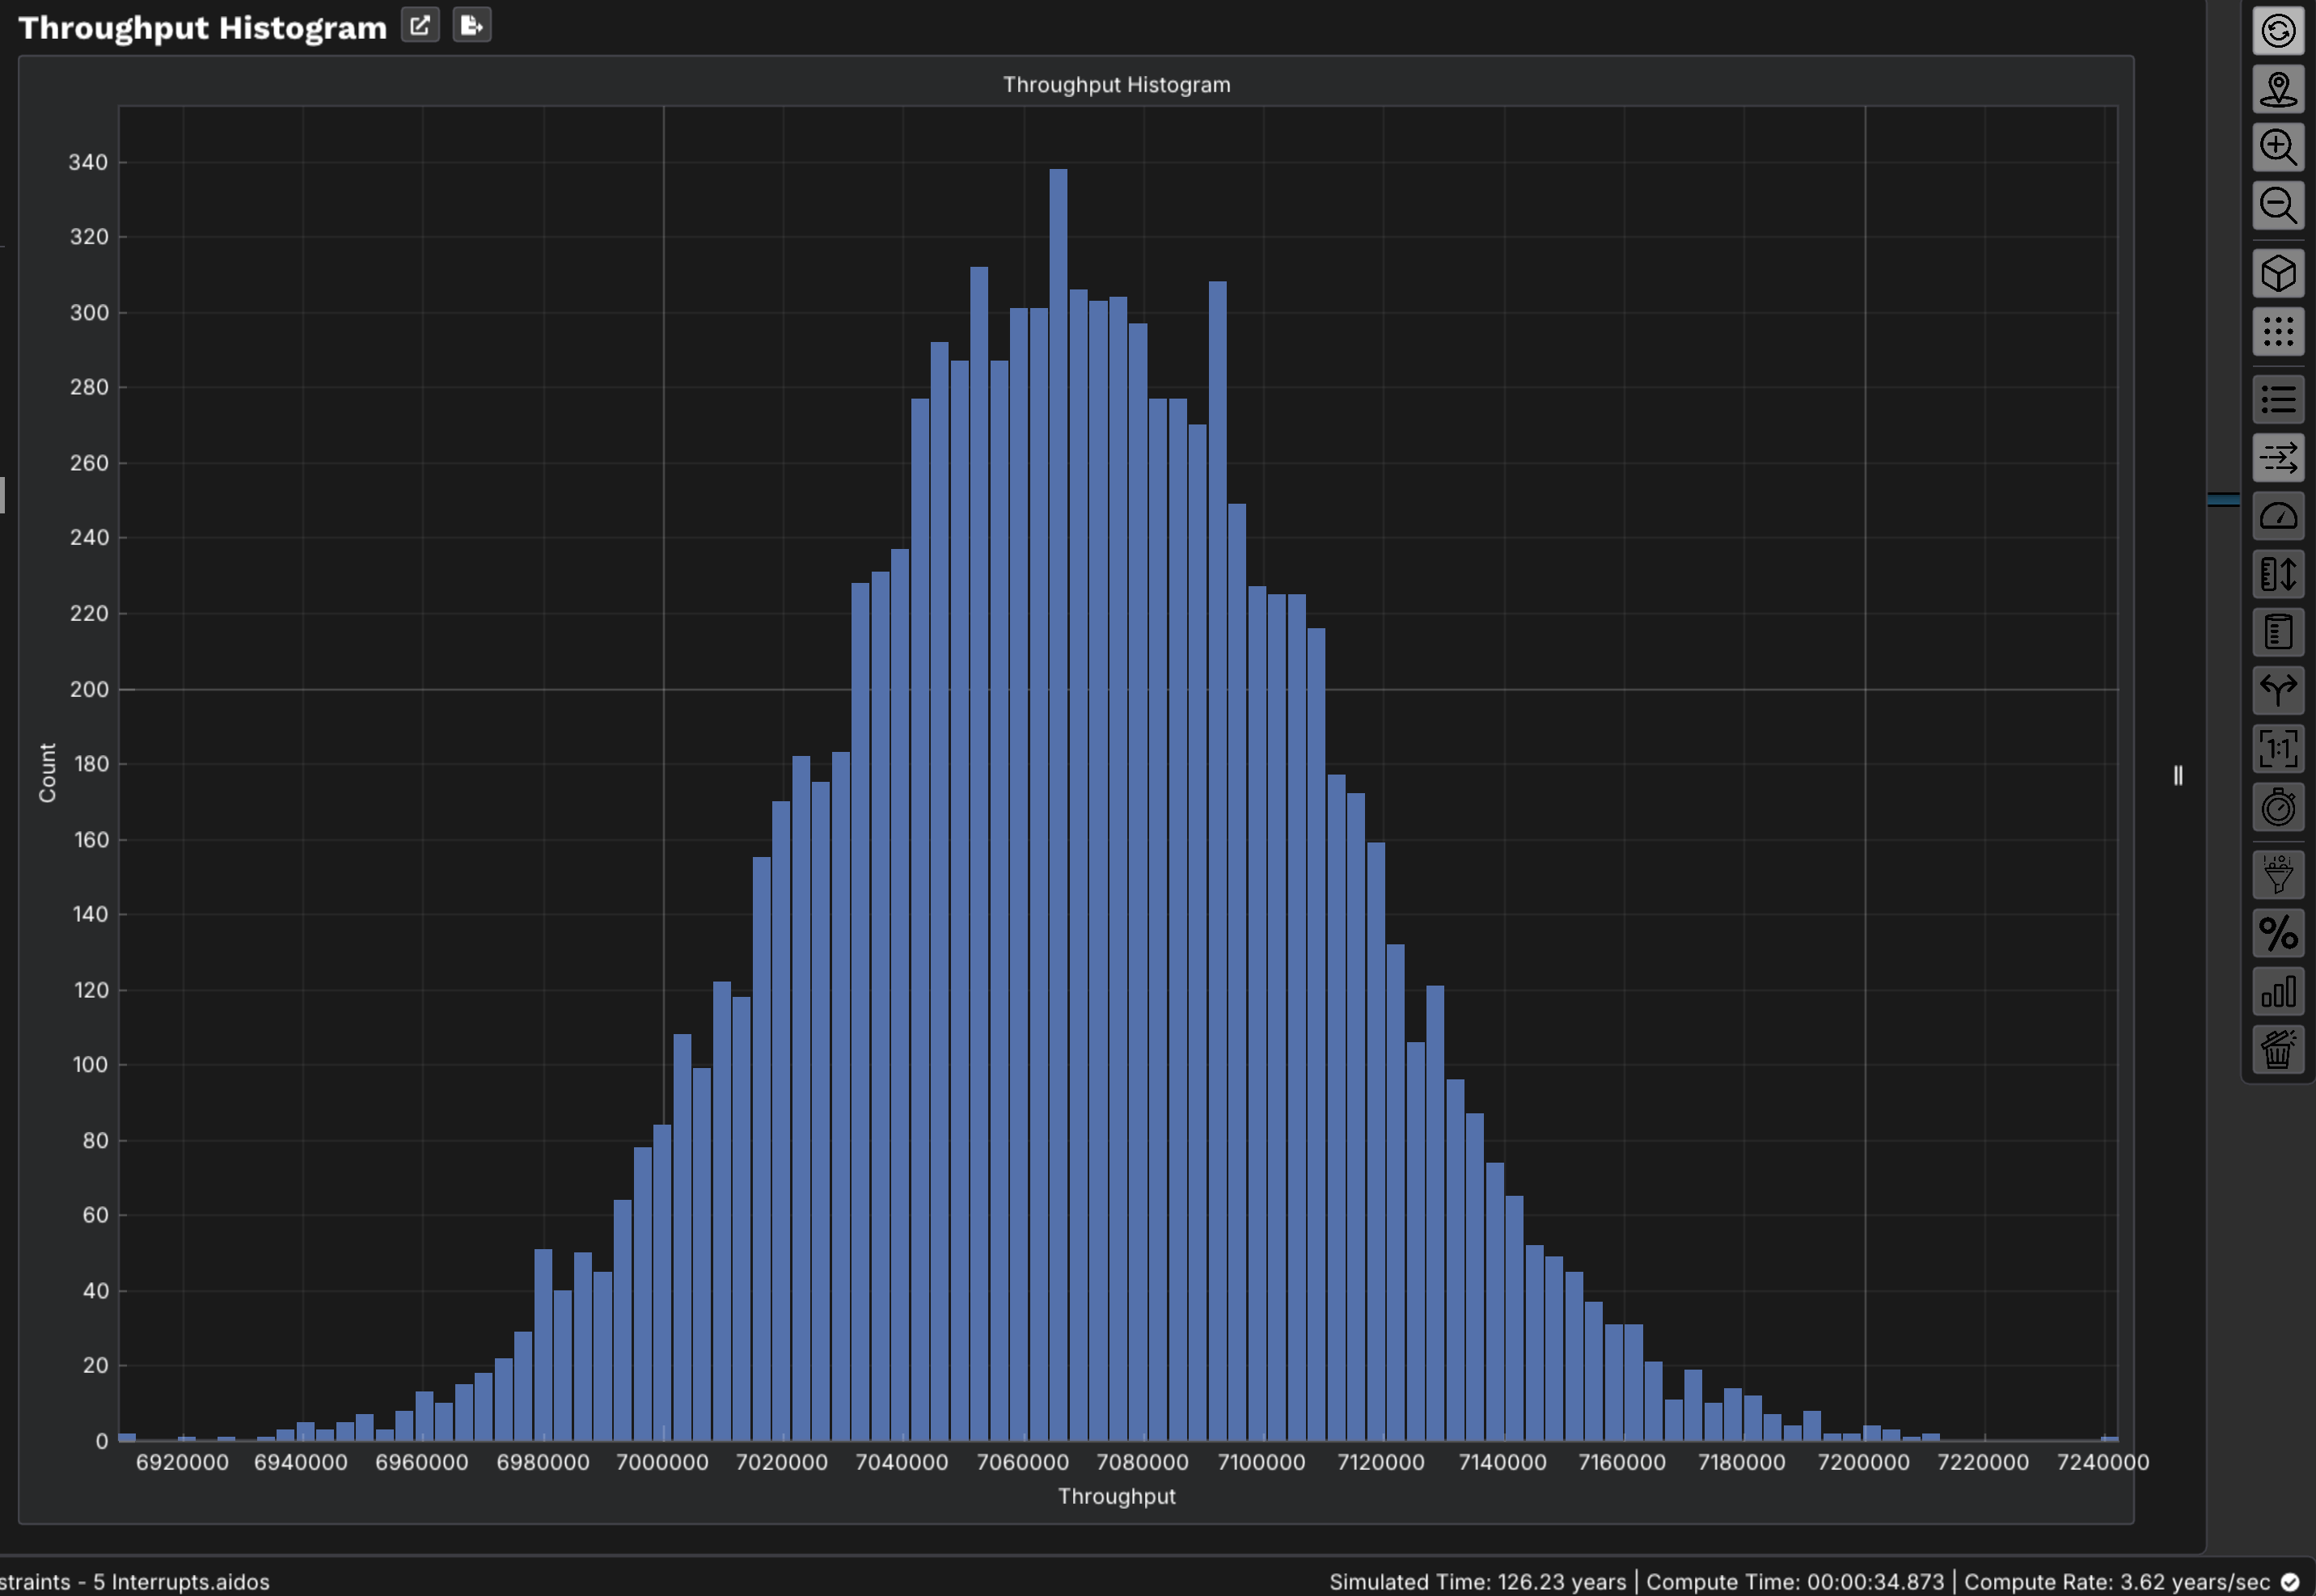
| The answer | One number | A distribution across replications |
| Best use | Screening many products and months quickly | Capital commitments, buffer sizing, peak-period capacity |
Both have a place. Use the spreadsheet for the first pass and simulation when coupling decides the answer. A major food manufacturer uses simulation to settle how many packaging lines to buy for a product line, where too few throttles a product and too many strands capital.
How a capacity study runs in ReliaSim®
1 · Build
Draw the line as it runs, or as proposed, with storage where it physically sits. Give each failure mode its distributions, either fitted by ReliaStats (downtime data analysis) or entered in the Interrupt Designer for a line that doesn’t exist yet. Turn every interrupt off and the model reports the most this topology can produce.
2 · Validate
Compare the model with the historian failure mode by failure mode before you trust it. The method has been validated within 1% of measured OEE on a real plant (published OEE validation).
3 · Predict
Change one thing at a time. Raise demand, add a machine, resize surge storage, change the changeover sequence, or remove a failure mode. Read capacity as a distribution across replications. Runs are cheap enough to compare candidate plans exhaustively instead of three picked in advance. The ReliaSim method covers each step.
Most of the project work above predates ReliaSim as a product. It was done with the discrete-rate method ReliaSim now packages, and each case study says which tool ran the model.
What simulation doesn’t replace
- A production schedule. A model can test a scheduling rule against variation before deployment, but writing tomorrow’s schedule is a planning system’s job.
- Rough-cut planning across the portfolio. Use simulation on the lines where coupling decides the answer.
- Data. The Interrupt Designer makes failure assumptions explicit, but it doesn’t make them right.
- Someone to build it. That’s manufacturing simulation consulting from ChiAha.
Frequently asked questions
What is capacity planning simulation?
It means modeling a production line or plant with its rates, storage, changeovers and per-failure-mode downtime. You then run it forward to see how much it produces under a given demand and mix, before capital or overtime is committed.
What’s the difference between rated capacity and effective capacity?
Rated capacity is what the machines can do while running, fed and unblocked. Effective capacity is what the line delivers after interrupts, blocking and starving, changeovers, rate losses and mix.
Can I plan capacity for a line that doesn’t exist yet?
Yes. Build the topology from the design, enter failure and repair distributions in the Interrupt Designer, and test configurations against demand. Validate the model against event data once the line runs.
Should we buy equipment, add overtime or improve reliability?
It depends on where the binding constraint is and how losses interact, which is what a simulation compares on one validated model. In several case studies on this site, the answer was a scheduling, storage or reliability change instead of new equipment.
What data does a capacity study need?
It needs machine stop and start times recorded to the second, ideally with named failure modes. It also needs nominal rates and conversions, the layout and storage capacities, and the demand or production plan with its changeovers.
How accurate is capacity planning simulation?
Close enough to act on, when built from per-failure-mode data and validated against line history. See the published OEE validation.
See capacity questions answered on a line model
The bottling-line models in the Sandbox’s Lines tier come with the engine’s saved results for each. On the Buffer-Options models you can see how much each buffer size adds and what the line gets back when each failure mode is removed. There’s nothing to download and no sign-up.
Open the Sandbox → Read the case studiesWant to see it on your own line? Schedule a call.